
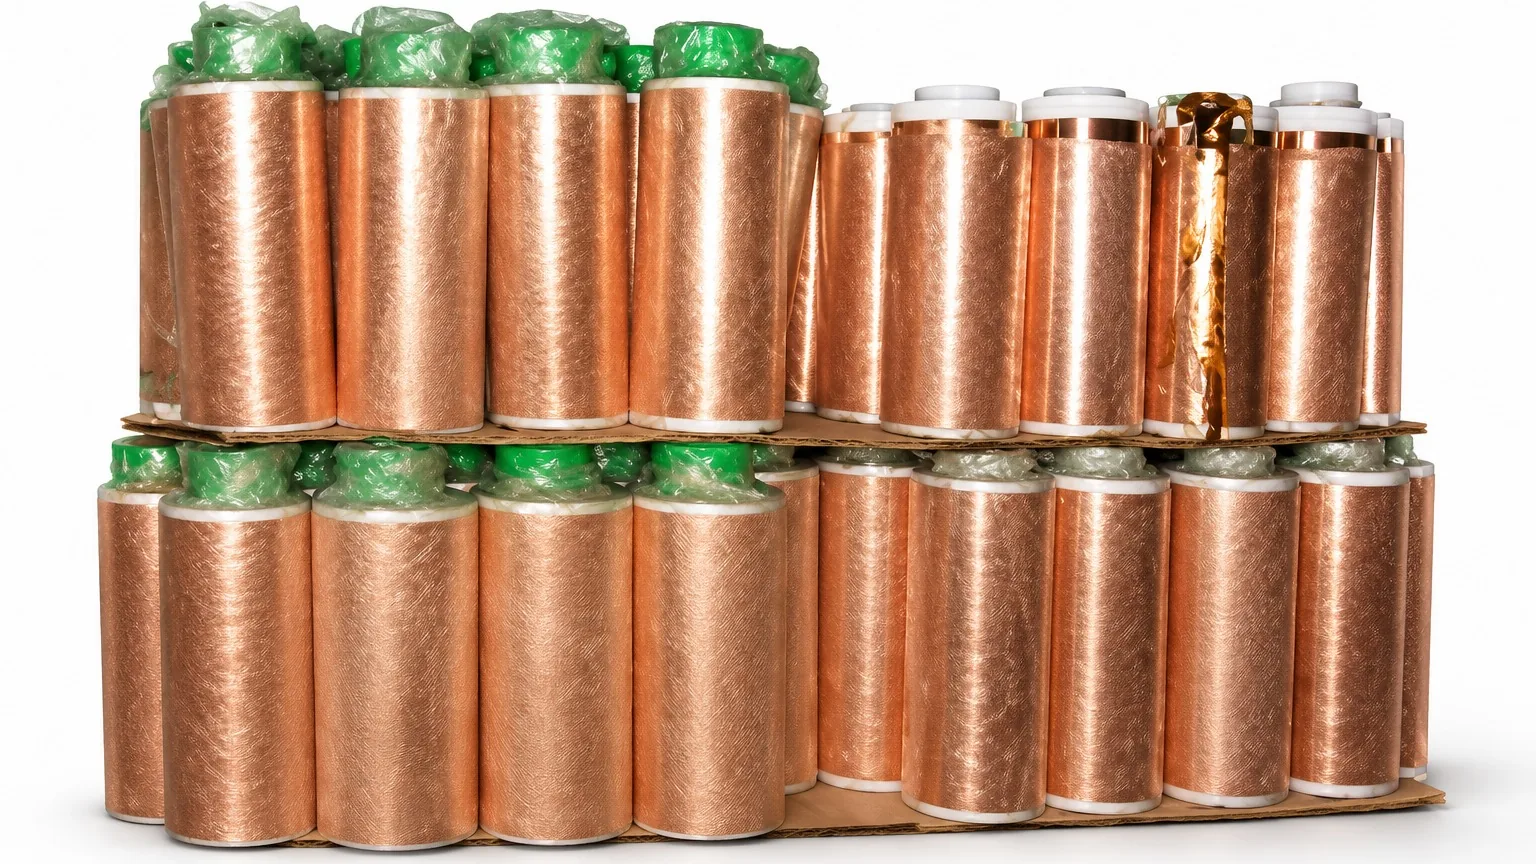
Copper foil may leave a cross-cutting machine at the programmed length yet still fail at the next operation. A sheet can carry wrinkles, edge tears, handling dents, contamination or curl. Thin foil can also shift during measurement, so a simple length check may hide a flatness or squareness problem.
This guide sets out a practical acceptance trial for copper foil. It starts with the required sheet, follows the material through the machine and identifies the documented HESPER configuration. It also separates published specifications from project-specific results that must be confirmed with the buyer's real roll.
1. Define the Accepted Copper Foil Sheet
Write the acceptance criteria before the trial. State target length and width, measurement datum, permitted variation, squareness method and the support surface used for inspection. Define acceptable edge burr, tearing, folded corners, scratches, dents, fingerprints and contamination. If one face is critical, identify it and explain how operators may touch or support it.
| Buyer concern | Evidence to record | Where to observe |
|---|---|---|
| Wrinkles or buckling | Both faces under consistent lighting | Roll release, pre-feeding, guidance and discharge |
| Length or squareness variation | Consecutive individual measurements | Feed contact, settings, cut and measurement method |
| Edge damage | Magnified edge photographs and reference samples | Incoming roll edge, guides, blade and handling |
| Curl or poor flatness | Sheet on the agreed support without hand tension | Incoming roll set, material path and collection |
Curl can originate in the supplied roll, while dents may be introduced during packing or manual collection. Record when each defect first appears.
2. Document the Production Roll
“Copper foil” is not a complete material specification. Record the supplier's grade or foil type, temper when provided, thickness, web width, roll outside diameter, core inside diameter, roll weight and winding direction. Add the surface finish, critical face, edge condition, splice locations and any protective or interleaving layer.
Use a representative production roll. A short hand-cut strip does not reproduce the edge condition or roll set of the intended input. Photograph the roll, label its orientation and retain a sample of the incoming edge.
3. Observe the Complete Material Path
Follow the roll from the separate roll stand to the spring-loaded pre-feeder, guides, polyurethane feed rollers, cross-cutting section and conveyor. The roll should release without abrupt drag or lateral wandering. Guides should control the web without scraping or folding an edge. Feed pressure should maintain contact without leaving an unacceptable impression.
At discharge, check whether the conveyor supports the sheet and preserves its orientation. Pieces may overlap, lift or receive damage when collected. Count handling time and rejected pieces as part of usable output.
4. Run a Traceable Cutting Trial
Use one documented setup and keep the samples in production order. A useful trial includes the following steps:
- Inspect the incoming roll for telescoping, loose winding, crushed areas, damaged edges, contamination and known splices.
- Record roll orientation, guide positions, roller-pressure settings, programmed length, speed, total quantity, batch quantity and pause time.
- Collect consecutive sheets near the beginning, middle and later portion of the test roll.
- Measure length and squareness with the same tools, datum, support and operator method.
- Inspect both faces, corners and cut edges under controlled lighting; record individual results rather than only an average.
- Repeat the checks after a normal stop and restart, and after a roll or length change when those events reflect production.
Link every adjustment to the first affected sample. A steady offset, gradual drift and isolated outlier suggest different causes. This traceability makes a trial more useful than a short video or one selected good sheet.
5. Match the Trial to HESPER's Documented Configuration
The HESPER Film, Paper and Fabric Cutting Machine with Spring-Loaded Pre-Feeder and Conveyor lists copper foil among its materials. Its documented process combines spring-loaded pre-feeding, cut-to-length cross-cutting and conveyor discharge. The Chinese/English LCD and keypad provide settings for length, speed, total quantity, batch quantity and pause time.
Published configuration includes Panasonic photoelectric sensing, polyurethane feed rollers with pressure adjustment at both ends, a separate bearing-supported roll stand, an SKD11 blade, a closed-loop cutting motor and cooling fans. CXY-300T, CXY-400T, CXY-500T and CXY-600T have listed working widths of 300, 400, 500 and 600 mm respectively.
The product data lists 0.01 mm feeding accuracy, 700 mm/s feed speed and 1.2 kW power. Feeding accuracy is not a guarantee of finished-sheet tolerance, and feed speed is not accepted production output. Confirm results with the actual foil thickness, roll condition, cut length, surface criteria and collection method. The HESPER unwind-roll specification guide helps buyers prepare the roll data needed before a trial.
6. Separate Cross-Cutting From Extra Processes
The documented machine feeds a roll, cross-cuts it to length and conveys the pieces. If the project also requires longitudinal slitting, edge trimming, protective interleaving, automated stacking, special clean handling or connection to another line, list each result separately. Do not assume those functions are standard.
Photoelectric sensing is documented, but the required detection target must be reviewed. Copper surfaces can be reflective, and any printed mark, gap or registration feature should be represented in the sample. Ask HESPER to confirm the proposed sensing method during the material trial.
Frequently Asked Questions
Does 0.01 mm feeding accuracy guarantee the same cut-length tolerance?
No. Finished results also depend on roll release, foil behaviour, feed contact, cutting and measurement. Approve consecutive measured samples against the buyer's own acceptance limits.
How should copper-foil flatness be checked?
Agree on a clean support surface, restraint method and measurement approach. Inspect samples without manually flattening them unless that exact method is part of the written acceptance rule.
Can the same setup handle every copper foil roll?
Do not assume so. Thickness, temper, surface, roll dimensions, winding quality and edge condition can change feeding and handling. Trial the actual production material.
What should a copper-foil cutting RFQ include?
Include foil identification, thickness, roll dimensions and weight; finished length and tolerance; edge and surface criteria; target usable output; collection needs; and sample availability.
Send HESPER a Measurable Copper Foil Requirement
Use the HESPER project enquiry to send the roll label, material photographs, finished-sheet drawing, defect limits and inspection method. HESPER can review the working width, material path, sensor target and trial plan before the machine configuration is confirmed.